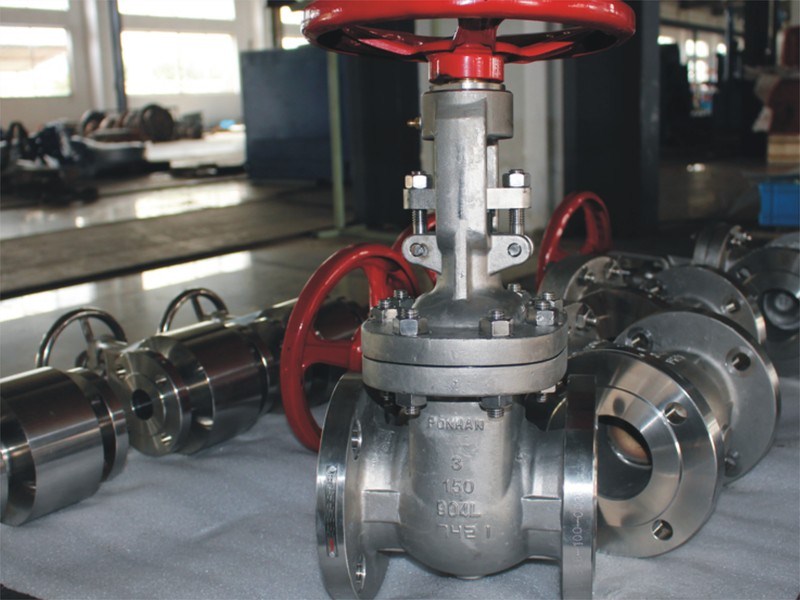
In the realm of industrial applications, the reliability and efficiency of components are paramount. Among these components, gate valves play a critical role in controlling the flow of fluids. Specifically, stainless steel gate valves have carved a niche for themselves due to their durability, corrosion resistance, and ability to withstand high-pressure environments. This article will explore the features, benefits, and applications of top-quality stainless steel gate valves, guiding industries in making informed decisions.
Features of Stainless Steel Gate Valves
Stainless steel gate valves are designed to provide robust performance across various industrial settings. Some of the key features include:
- Corrosion Resistance: The stainless steel construction offers excellent resistance to corrosive environments, making these valves suitable for applications involving harsh chemicals and extreme conditions.
- High-Pressure Tolerance: These valves can withstand high pressure, ensuring safety and reliability in demanding applications.
- Temperature Resilience: Capable of functioning efficiently across a wide range of temperatures, stainless steel gate valves are versatile components in many industrial processes.
- Durability: The robust construction of these valves ensures a long service life, reducing the need for frequent replacements.
Benefits of Using Stainless Steel Gate Valves
Utilizing stainless steel gate valves in industrial applications offers several advantages:
- Reliability: With their ability to maintain integrity under stress, these valves provide consistent performance, minimizing the risk of leaks and failures.
- Cost-Effectiveness: The durability and extended service life contribute to reduced maintenance costs and downtime.
- Versatility: Suitable for a wide range of applications, including water treatment, oil and gas, and chemical processing.
- Ease of Maintenance: Simple design and construction facilitate easy maintenance and repair, ensuring minimal operational disruption.
Applications of Stainless Steel Gate Valves
Oil and Gas Industry
The oil and gas sector relies heavily on stainless steel gate valves due to their ability to handle high pressures and corrosive substances. These valves are integral in controlling the flow of crude oil and natural gas.
Chemical Processing
In chemical plants, the durability and corrosion resistance of stainless steel gate valves ensure safe operation in environments where chemicals can otherwise cause significant damage to other materials.
Water Treatment Facilities
Gate valves play a crucial role in water treatment facilities, where they regulate the flow of water and other treatments. The stainless steel construction ensures long-term reliability and minimizes the risk of contamination.
Considerations When Choosing Stainless Steel Gate Valves
When selecting a stainless steel gate valve for industrial applications, several factors should be considered to ensure optimal performance:
- Pressure Rating: Evaluate the pressure requirements of the application to select a valve with appropriate specifications.
- Temperature Range: Ensure the valve can operate efficiently within the expected temperature range of the application.
- Size and Compatibility: Consider the size and compatibility with existing systems to ensure seamless integration.
- Quality Standards: Verify that the valve meets relevant industry standards for safety and performance.
In conclusion, stainless steel gate valves are an indispensable component in various industrial applications. Their combination of strength, durability, and resistance to harsh conditions makes them a wise choice for industries striving for efficiency and reliability. By carefully considering the specific needs of the application, industries can select the most suitable valve, ensuring long-term success and operational excellence.